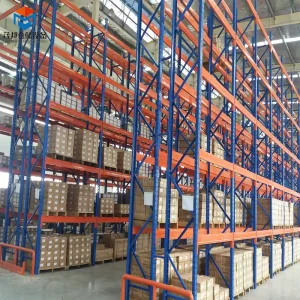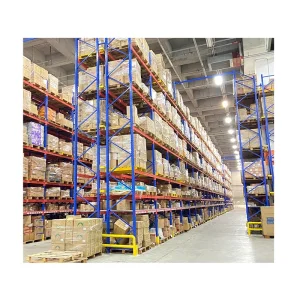
As global supply chains navigate unprecedented transformations, the demand for high-performance industrial storage and heavy-duty shelving has reached historical peaks. Modern distribution centers, automated warehousing facilities, and large-scale manufacturing ecosystems require robust, scalable, and seismically certified storage infrastructures. As a premier provider from China, Guangdong Maobang Storage Equipment Co., Ltd. sits at the bleeding edge of this industrial evolution, delivering engineered storage solutions that combine maximum load capacity, spatial optimization, and uncompromising structural integrity.
Understanding search intent and semantic depth in industrial engineering requires analyzing operational friction points. Enterprise buyers no longer seek generic storage racks; they demand fully customizable, compliant, and precision-manufactured systems capable of withstanding rigorous operational cycles. This white paper explores our advanced production technology, stringent quality assurance paradigms, and localized deployment strategies designed to empower global businesses.
Guangdong Maobang Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse racking systems, industrial storage solutions, and customized storage equipment. Founded in 2016, the company has developed into a reliable storage equipment supplier with strong manufacturing capabilities, advanced production technology, and extensive export experience.
With a factory area of approximately 18,500㎡, Maobang Storage Equipment focuses on providing high-quality storage solutions for warehouses, logistics centers, factories, and commercial facilities worldwide. The company achieves an annual export revenue of around USD 18 million and has accumulated 7 years of export experience and 12 years of industry experience.
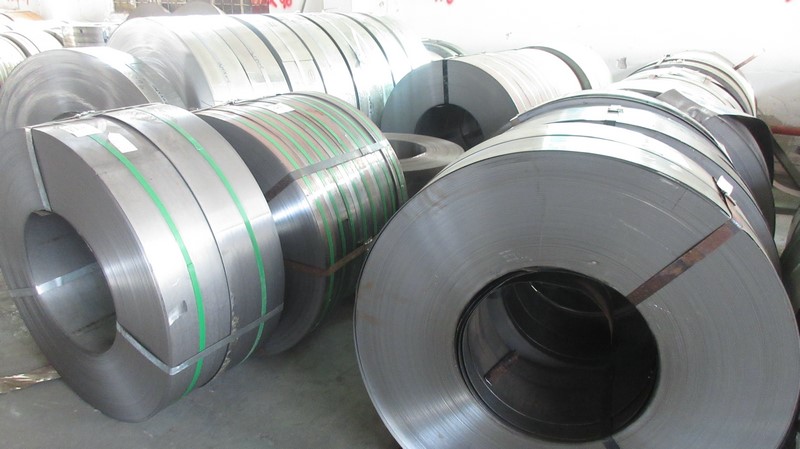
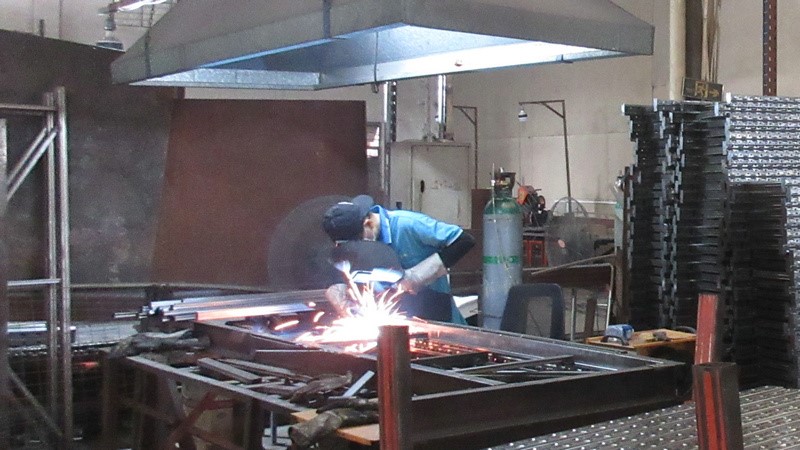
The company operates a strict quality management system with professional inspection procedures, including raw material testing, welding inspection, surface coating inspection, load capacity testing, and finished product evaluation. Quality inspections are conducted through automated testing equipment combined with manual quality checks to ensure product reliability and safety. The dedicated quality control team consists of 45 professional inspectors who monitor every stage from production to final shipment.
Maobang Storage Equipment has rich international trade experience and serves customers across North America, Europe, Southeast Asia, the Middle East, South America, and Oceania. The company has established stable cooperation with more than 850 supply chain partners, ensuring efficient material sourcing, production stability, and timely delivery.
The company mainly serves warehouse operators, logistics companies, manufacturing enterprises, retail businesses, distributors, and engineering contractors. With strong R&D capabilities, Maobang continuously develops innovative storage products and optimized warehouse solutions to meet changing market demands.
Customers can choose from a wide range of customization options, including size customization, load capacity design, color selection, structure optimization, and complete warehouse layout planning. In the past year, Maobang launched 120 new products to improve storage efficiency and provide more flexible solutions.
The company has a professional R&D team consisting of 85 experienced engineers dedicated to product innovation, structural improvement, and customized project development. Through continuous investment in technology and quality improvement, Guangdong Maobang Storage Equipment Co., Ltd. aims to become a trusted global partner for advanced warehouse storage solutions.
Heavy-duty shelving and selective pallet racking systems are not one-size-fits-all products. Different geographic regions and industry verticals impose unique structural, seismic, and environmental requirements:
As the industrial sector transitions toward Industry 4.0, Maobang's engineering roadmap incorporates cutting-edge advancements:
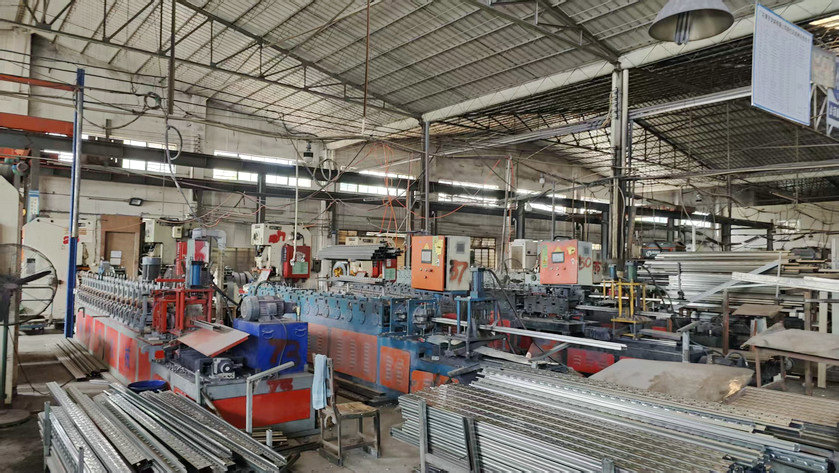
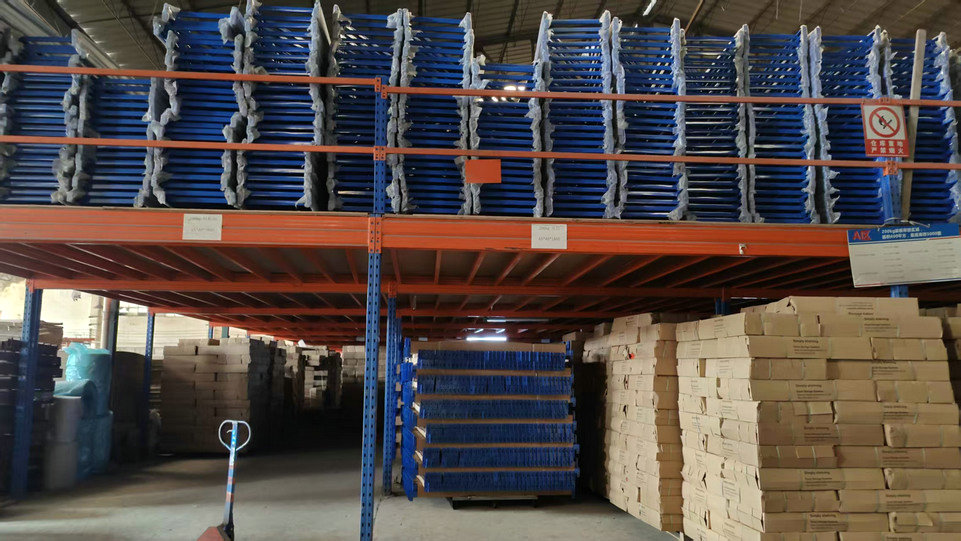
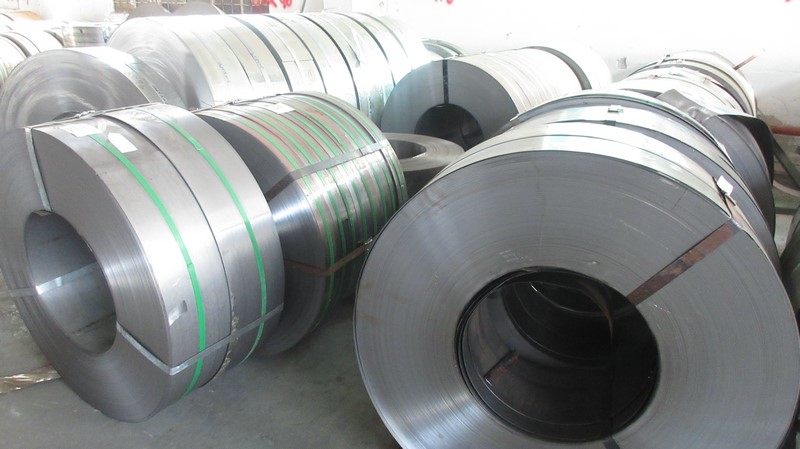
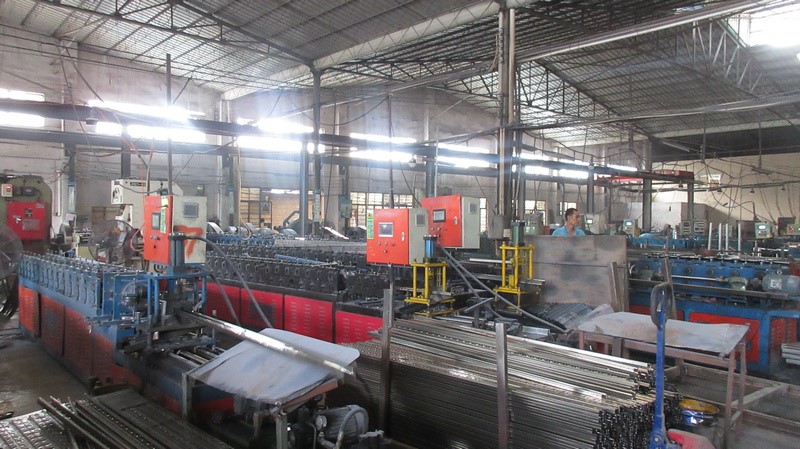
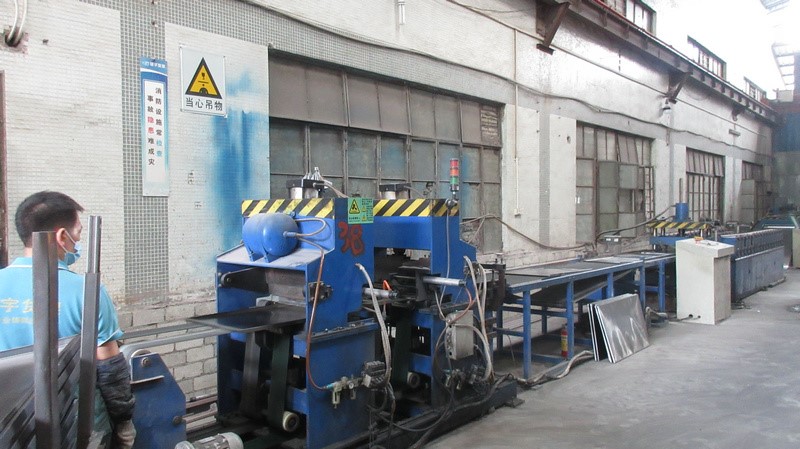
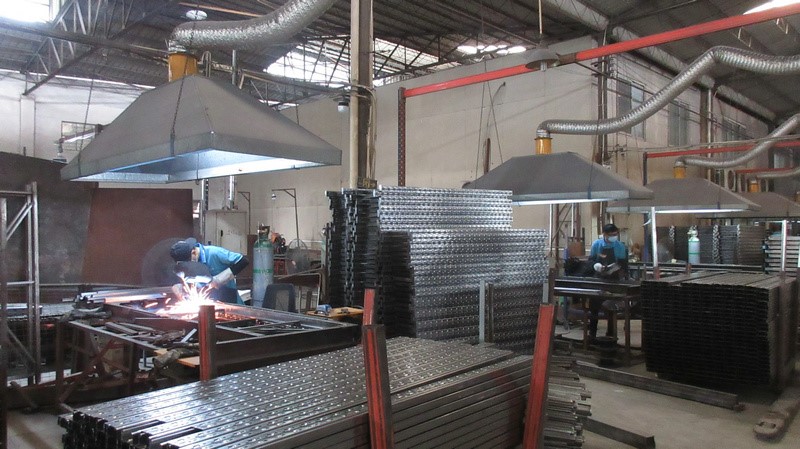
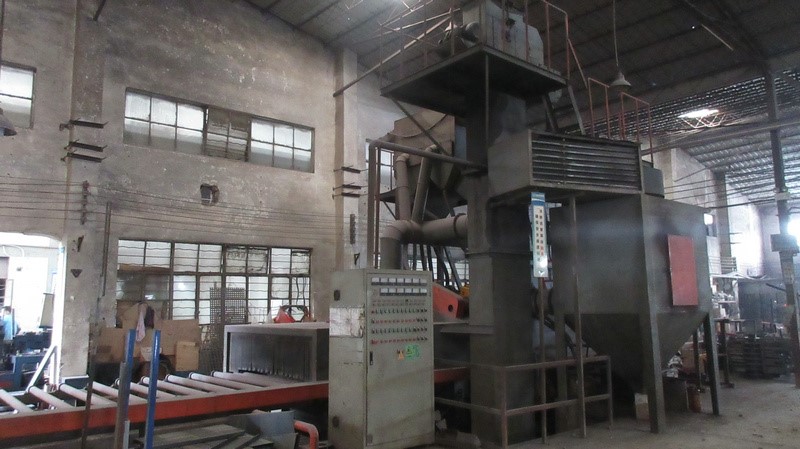
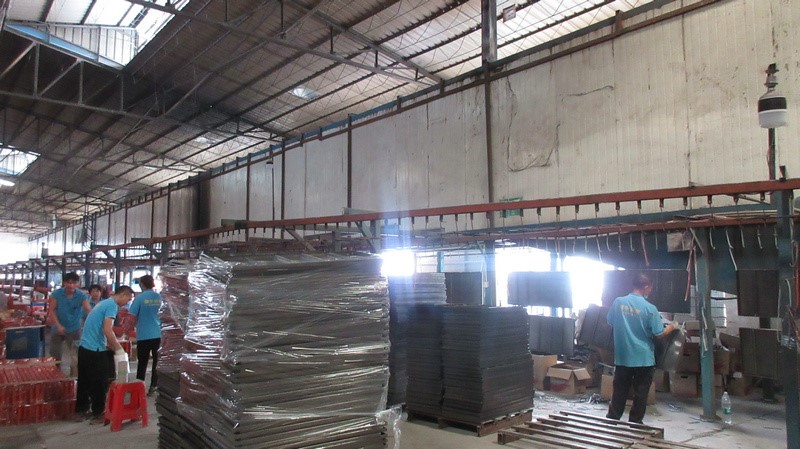
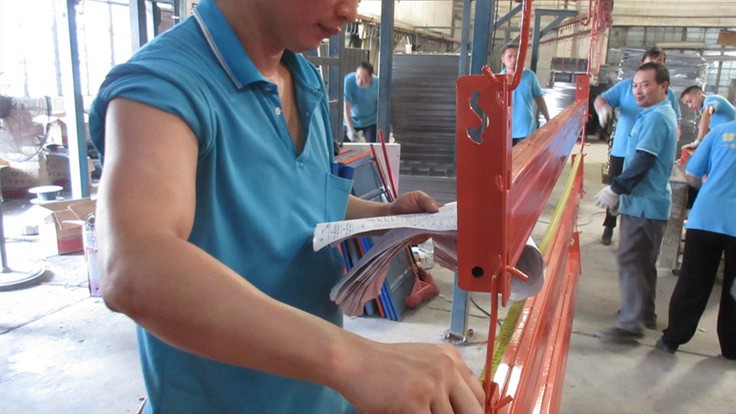
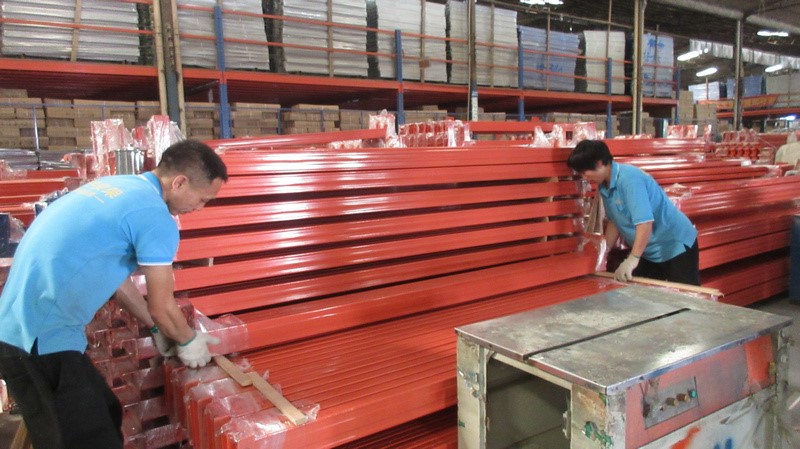
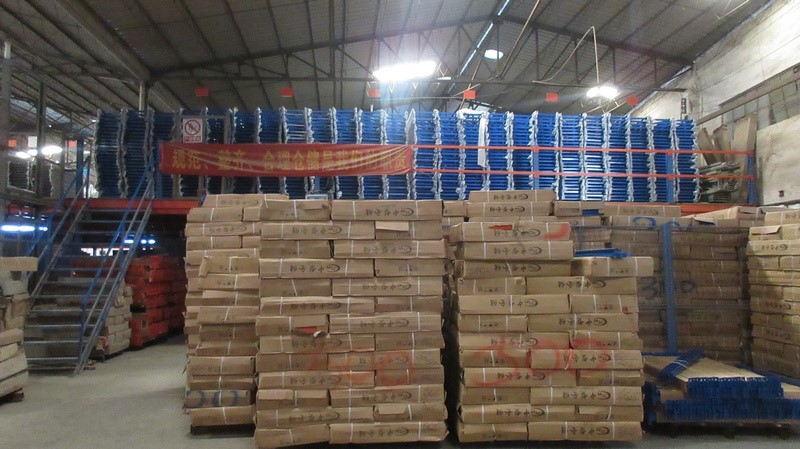
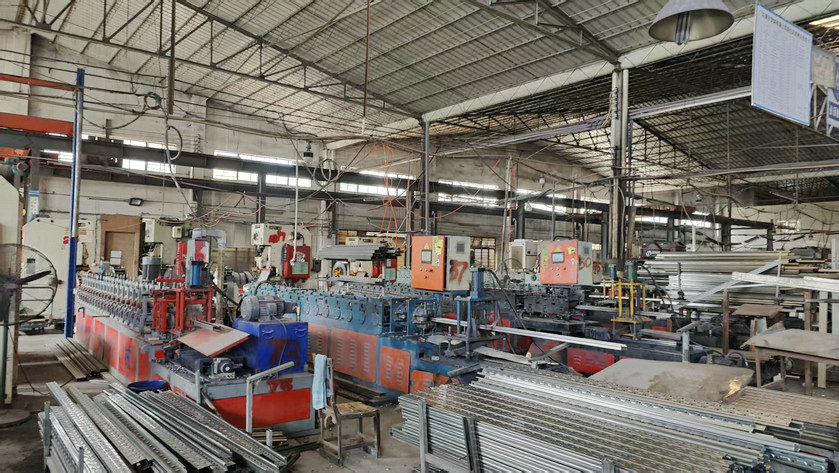
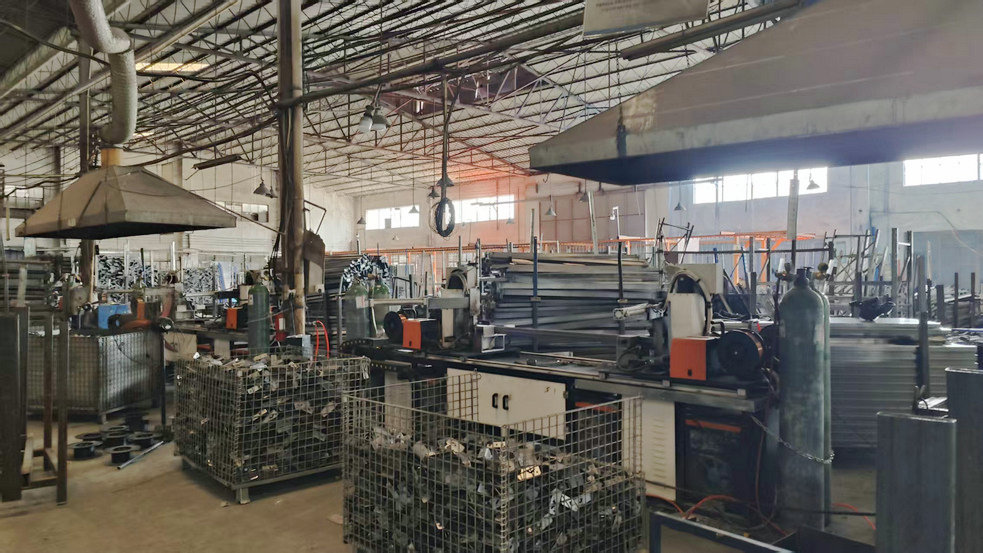
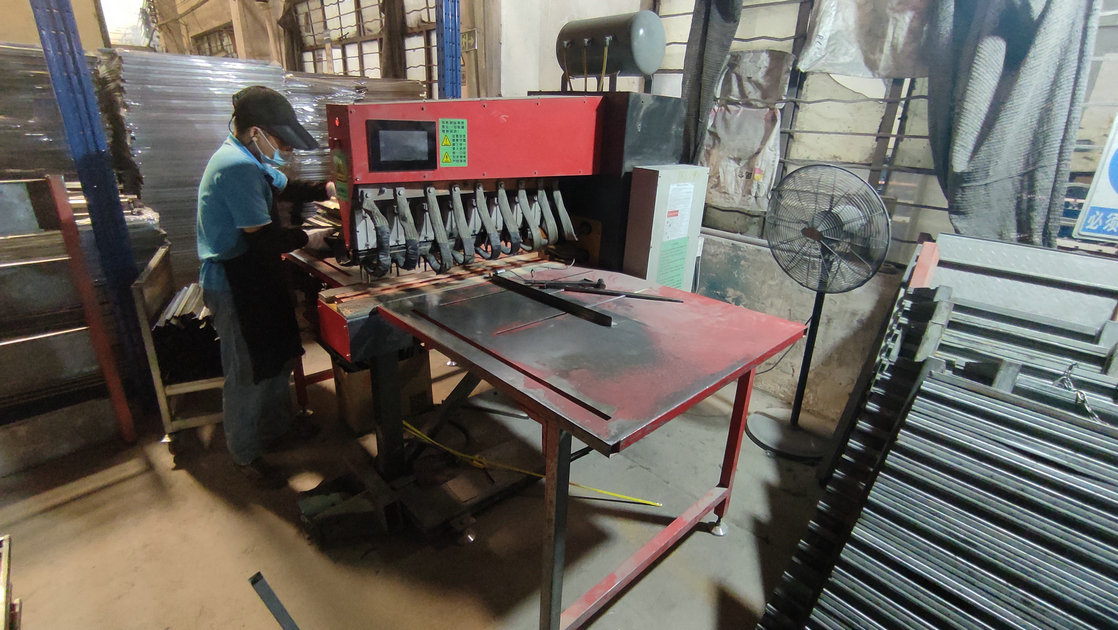
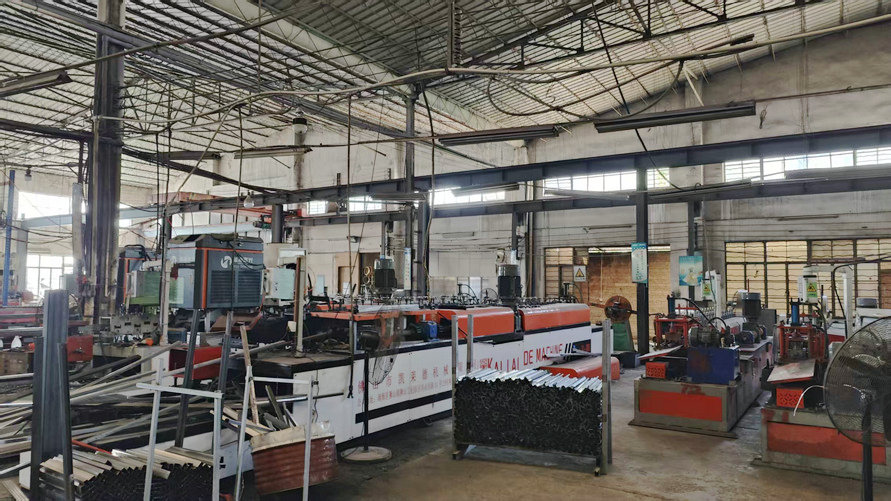
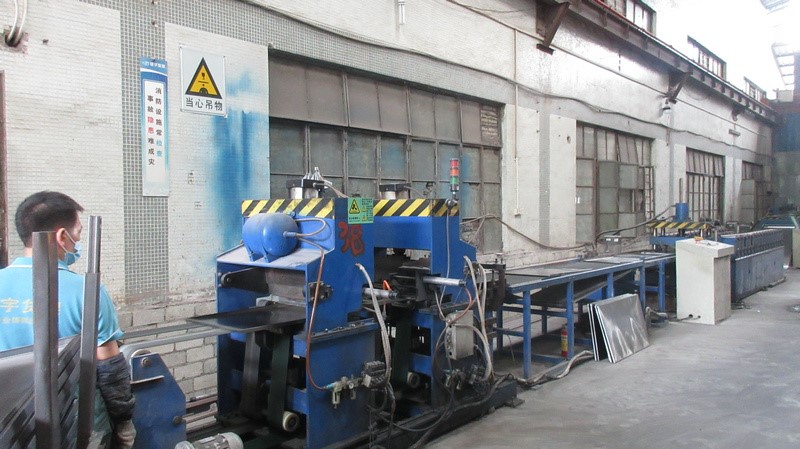
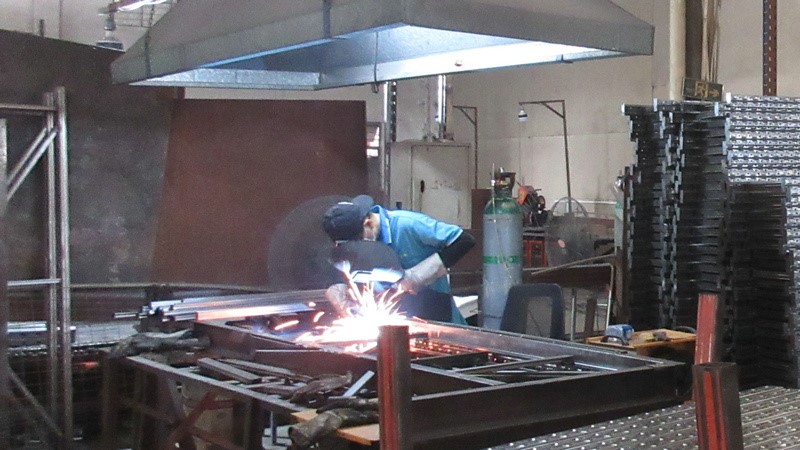
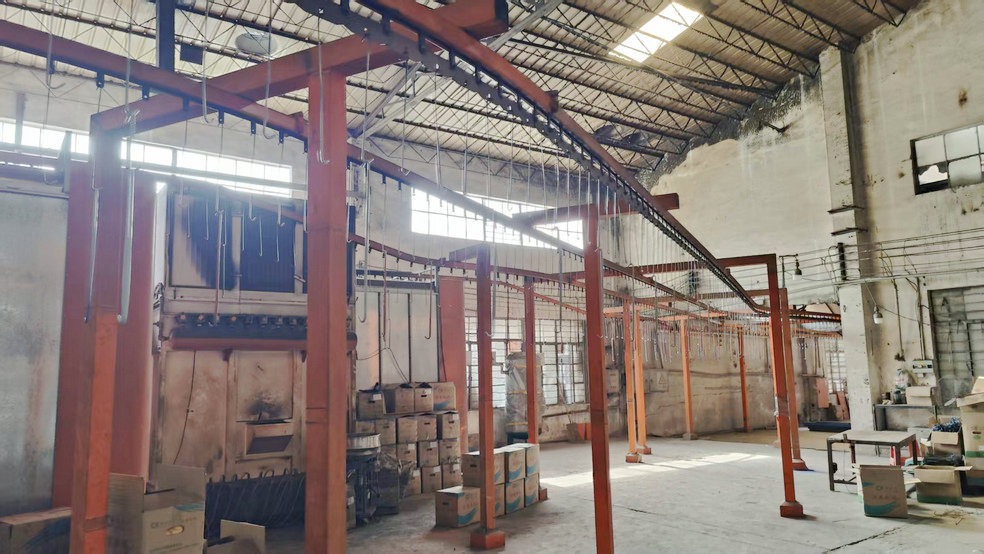
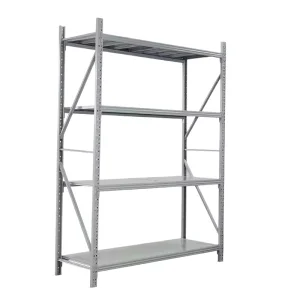
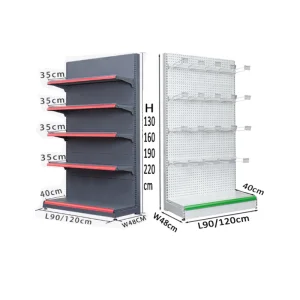
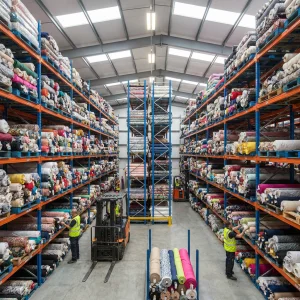
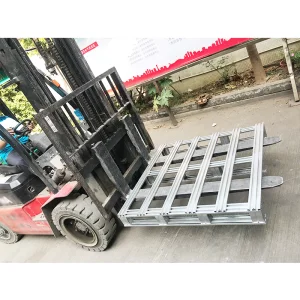
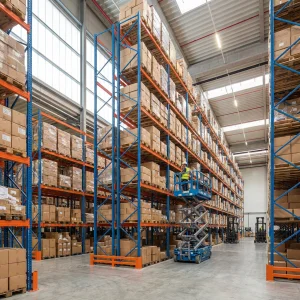
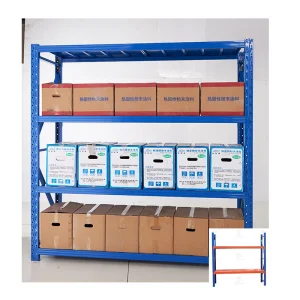
With over 12 years of industry expertise, an 18,500㎡ state-of-the-art facility, 85 specialized R&D engineers, and a dedicated team of 45 quality inspectors, we deliver factory-direct pricing, strict ISO-compliant quality control, and robust global logistics support across 850+ supply chain partnerships.
Yes! We specialize in comprehensive structural customization, including tailored height and depth dimensions, load capacity calculations, color coding, and complete 3D warehouse layout planning to optimize your cubic storage efficiency.
Our products undergo rigorous testing procedures—including raw material inspection, automated welding analysis, surface coating thickness checks, and destructive load capacity testing—ensuring compliance with international safety benchmarks for North American, European, and Asian markets.
Thanks to our advanced automated cutting and bending machinery and stable raw material supply chains, standard production lead times range from 15 to 25 days depending on project scale and specific customization requirements.
 Maobang Storage