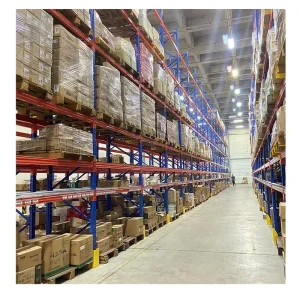
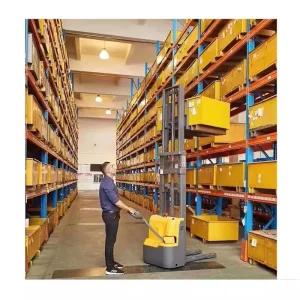
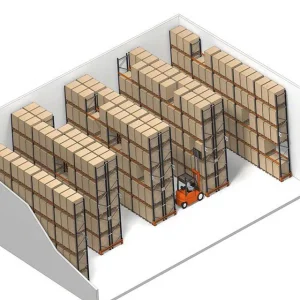
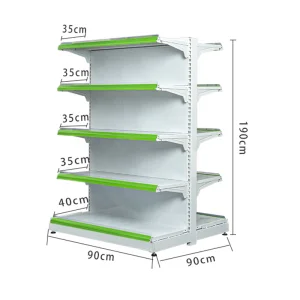
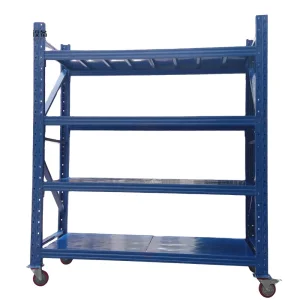
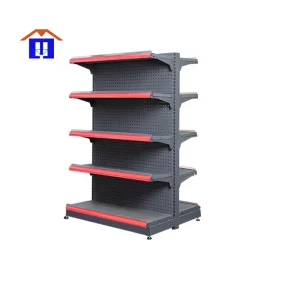
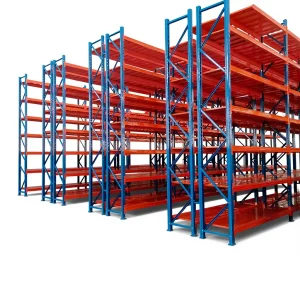
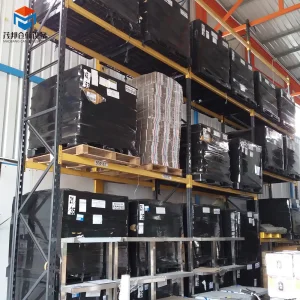
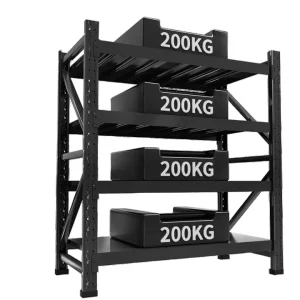
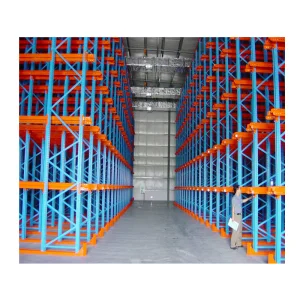
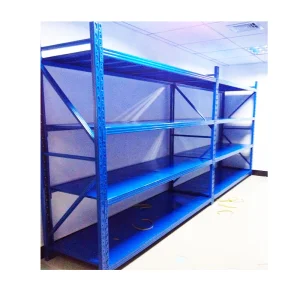
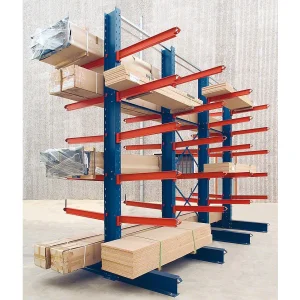
Guangdong Maobang Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse racking systems, industrial storage solutions, and customized storage equipment. Founded in 2016, the company has developed into a reliable storage equipment supplier with strong manufacturing capabilities, advanced production technology, and extensive export experience.
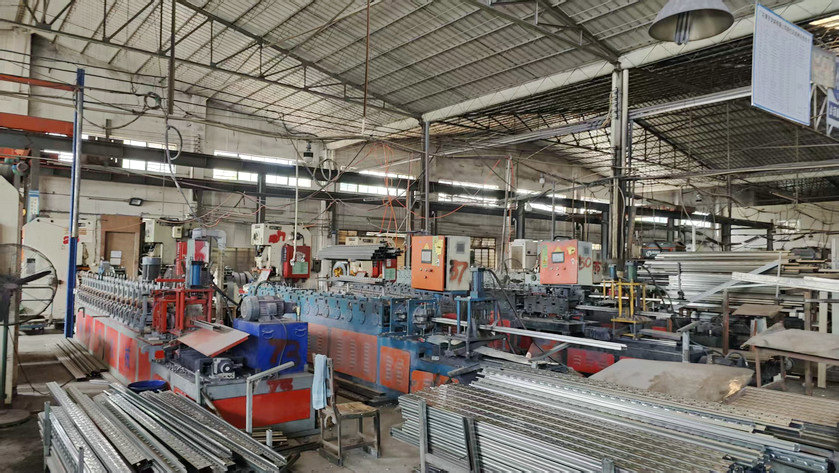
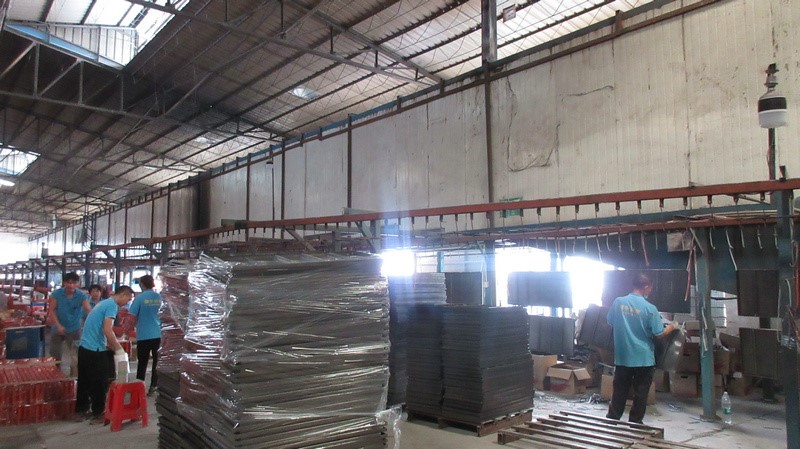
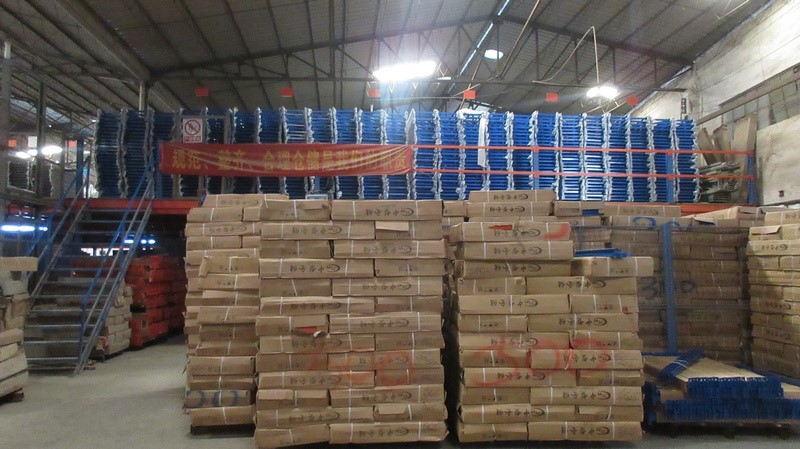
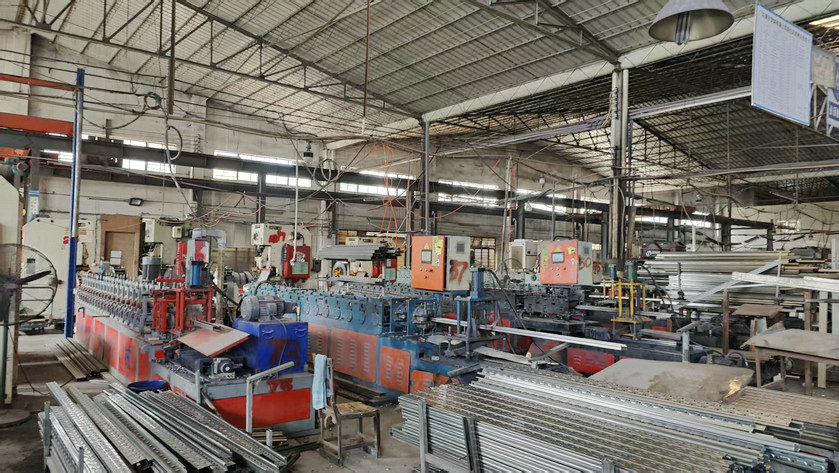
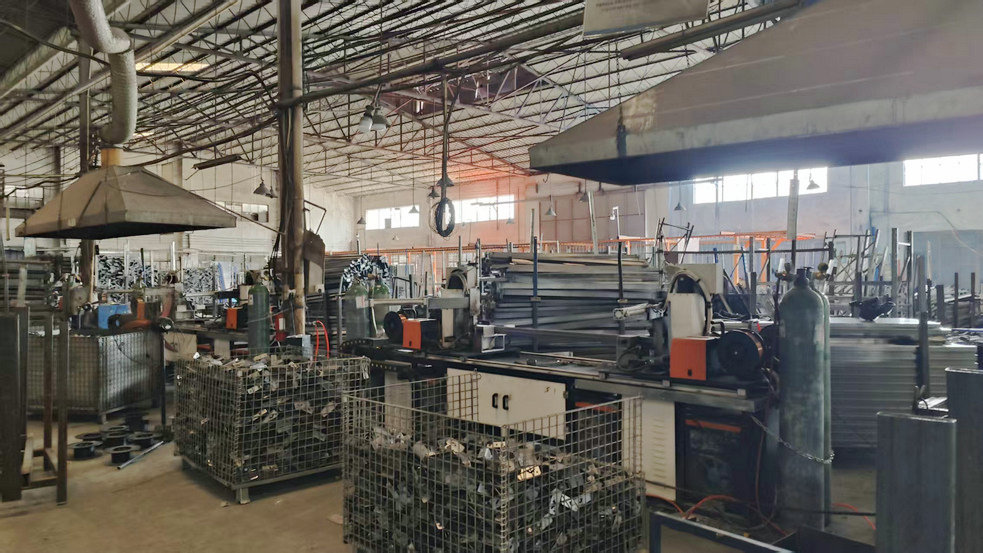
With a factory area of approximately 18,500㎡, Maobang Storage Equipment focuses on providing high-quality storage solutions for warehouses, logistics centers, factories, and commercial facilities worldwide. The company achieves an annual export revenue of around USD 18 million and has accumulated 7 years of export experience and 12 years of industry experience.
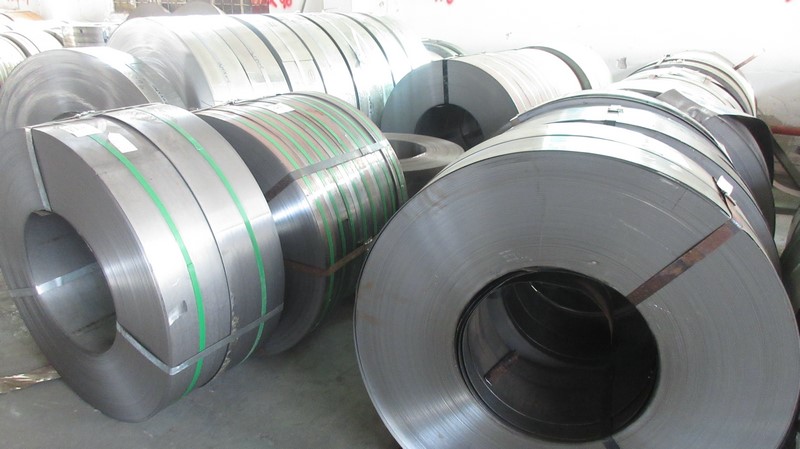
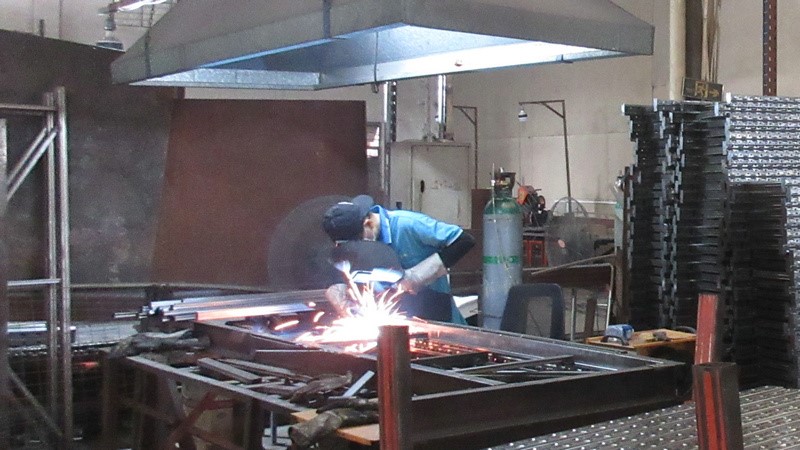
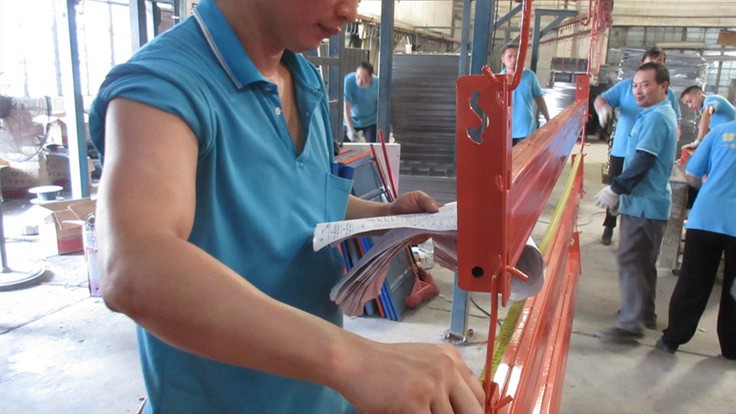
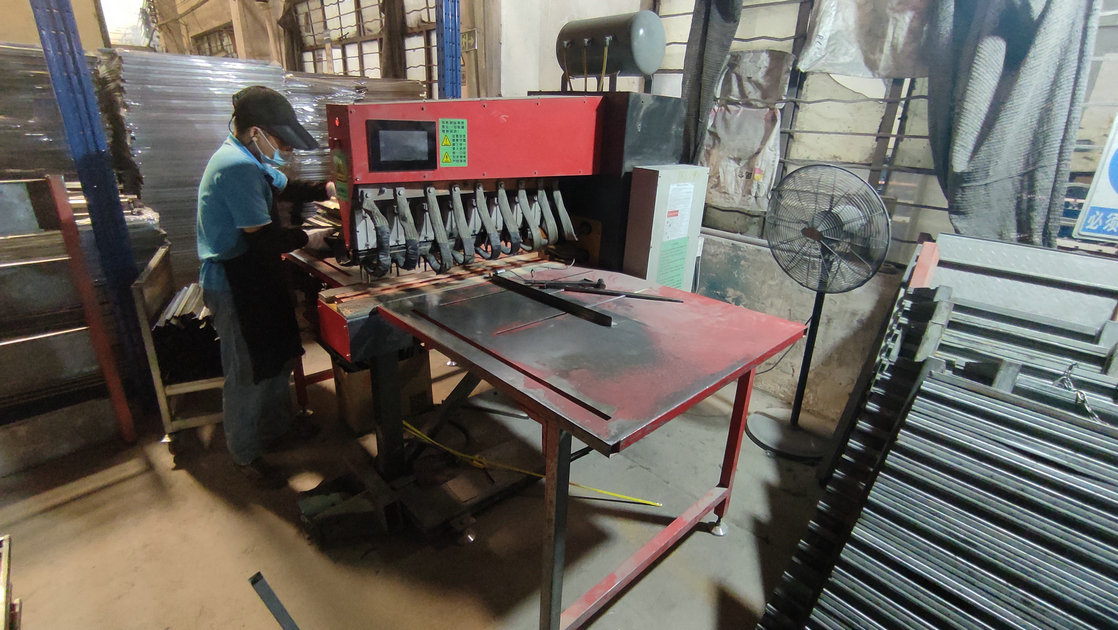
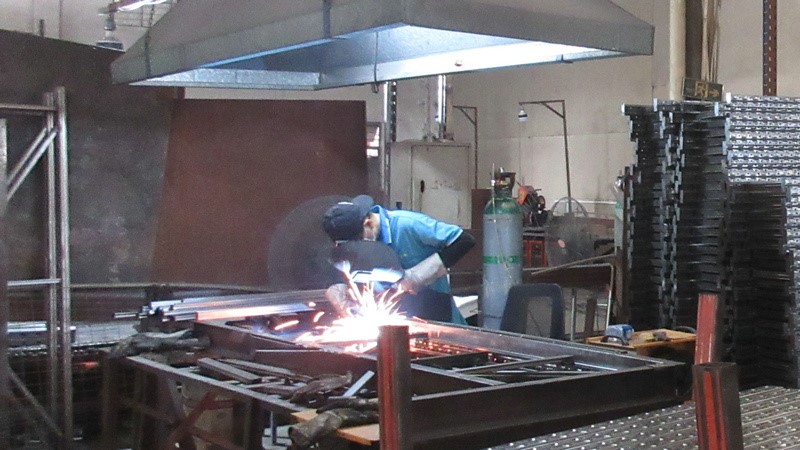
The company operates a strict quality management system with professional inspection procedures, including raw material testing, welding inspection, surface coating inspection, load capacity testing, and finished product evaluation. Quality inspections are conducted through automated testing equipment combined with manual quality checks to ensure product reliability and safety. The dedicated quality control team consists of 45 professional inspectors who monitor every stage from production to final shipment.
Maobang Storage Equipment has rich international trade experience and serves customers across North America, Europe, Southeast Asia, the Middle East, South America, and Oceania. The company has established stable cooperation with more than 850 supply chain partners, ensuring efficient material sourcing, production stability, and timely delivery.
The company mainly serves warehouse operators, logistics companies, manufacturing enterprises, retail businesses, distributors, and engineering contractors. With strong R&D capabilities, Maobang continuously develops innovative storage products and optimized warehouse solutions to meet changing market demands.
Customers can choose from a wide range of customization options, including size customization, load capacity design, color selection, structure optimization, and complete warehouse layout planning. In the past year, Maobang launched 120 new products to improve storage efficiency and provide more flexible solutions.
The company has a professional R&D team consisting of 85 experienced engineers dedicated to product innovation, structural improvement, and customized project development. Through continuous investment in technology and quality improvement, Guangdong Maobang Storage Equipment Co., Ltd. aims to become a trusted global partner for advanced warehouse storage solutions.
Information Gain Notice: Gravity Flow Racks leverage high-density FIFO (First-In, First-Out) principles, optimizing cubic space utilization by up to 60% compared to traditional selective pallet racking systems.
In the modern era of omni-channel distribution and high-velocity supply chains, warehouse managers face unprecedented pressure to reduce footprint costs while maximizing picking throughput. Gravity flow racks represent an engineering pinnacle in high-density storage. Utilizing inclined roller tracks and controlled braking systems, pallets or cartons glide effortlessly via gravitational force from the loading aisle to the picking aisle.
From cold storage facilities in Northern Europe requiring corrosion-resistant galvanized finishes to heavy automotive manufacturing plants in North America demanding extreme structural load capacities, Maobang’s gravity flow racking architectures adapt seamlessly to regional environmental parameters and regulatory building codes (such as RMI and FEM standards).
Integrating IoT-enabled smart sensors onto gravity flow tracks enables real-time inventory tracking, predictive maintenance, and automated stock-flow analytics. Our R&D roadmap emphasizes lightweight high-strength steel alloys and frictionless composite roller bearings, reducing operational wear and enhancing long-term durability.
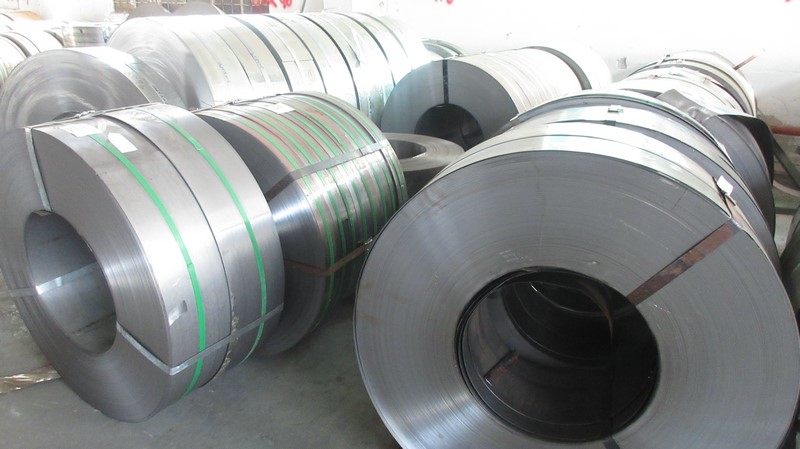
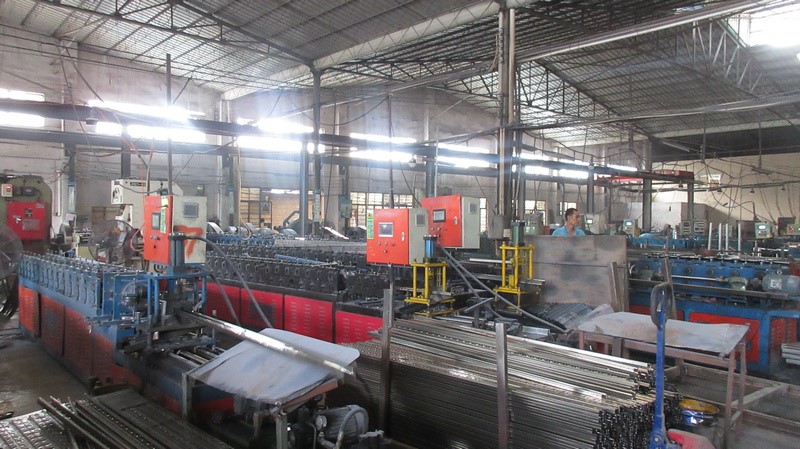
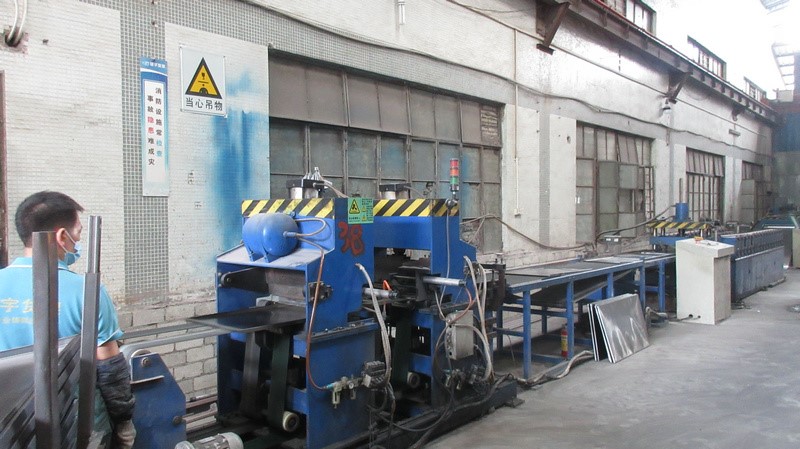
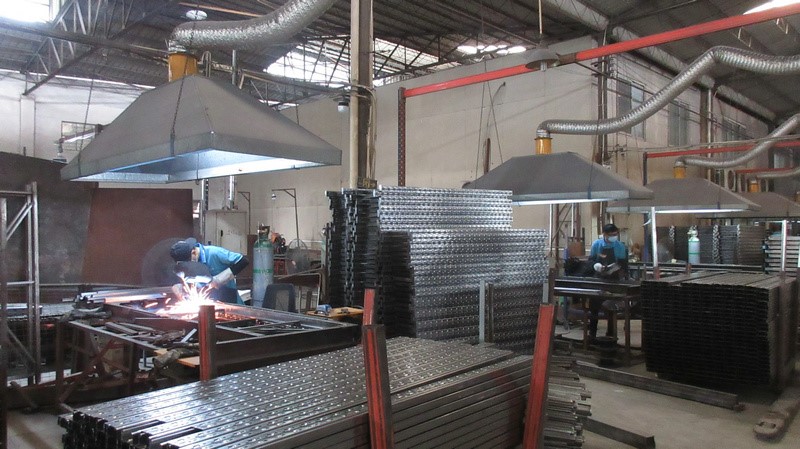
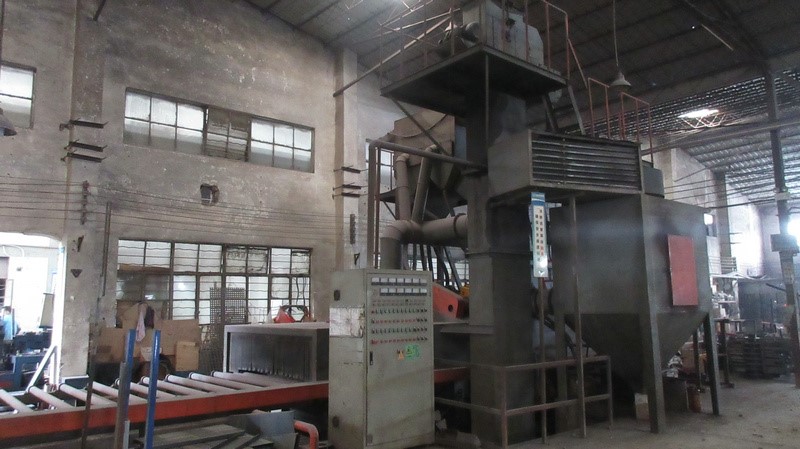
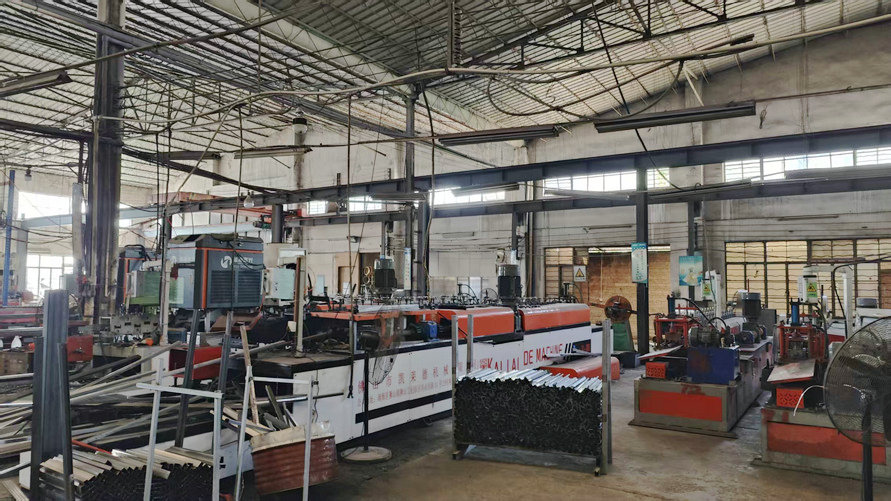
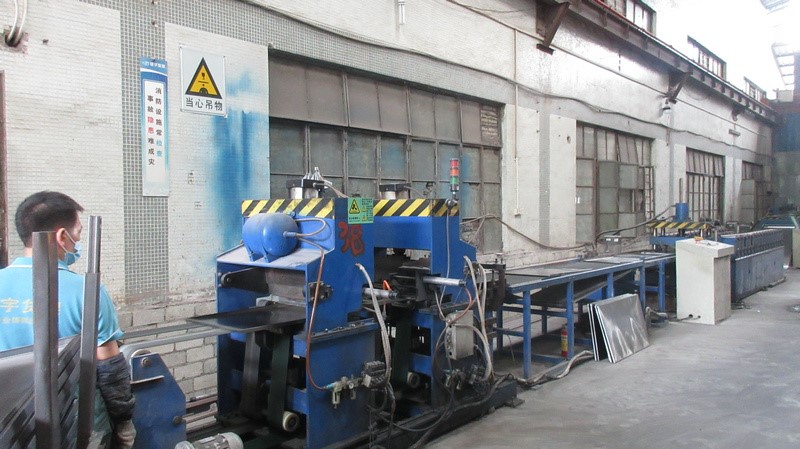
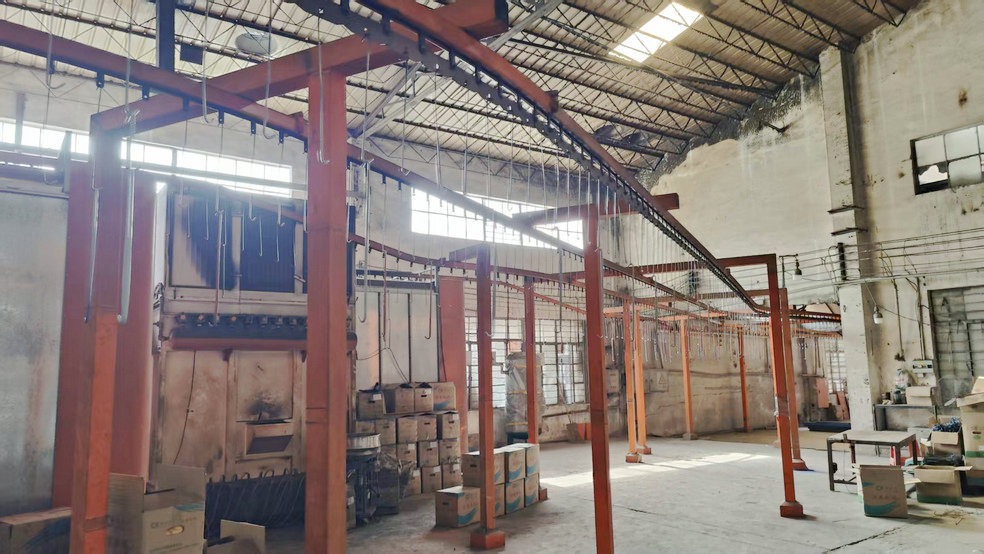
Our 18,500㎡ facility incorporates automated robotic cutting units, CNC bending machinery, and advanced electrostatic powder coating lines. This vertical integration guarantees absolute supply chain continuity, competitive wholesale pricing, and uncompromised quality control.
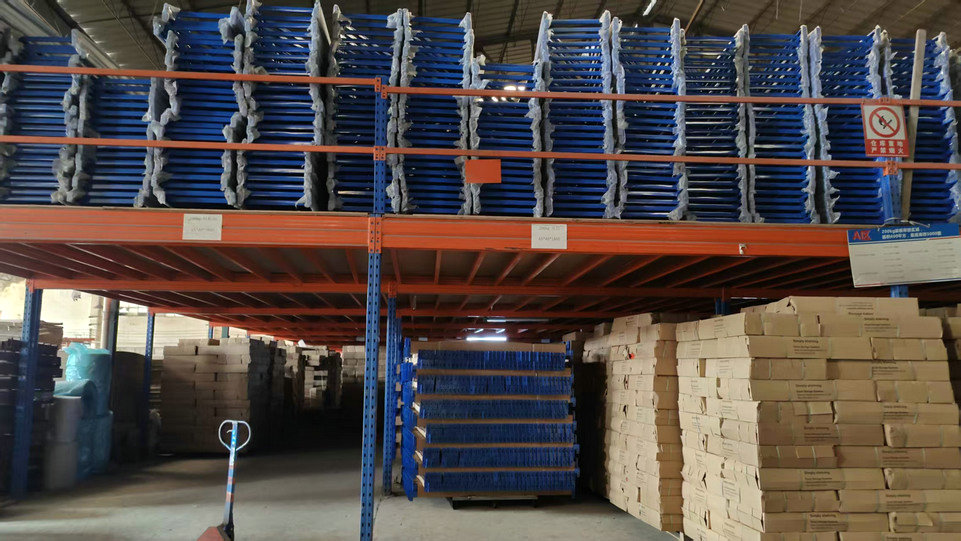
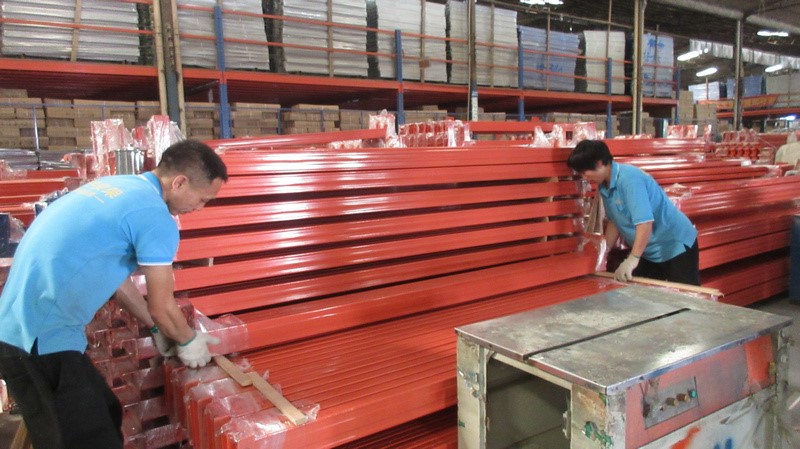
Gravity flow racks provide significantly higher space utilization by operating on a FIFO (First-In, First-Out) principle with high-density storage lanes. This reduces aisle space requirements by up to 50% and dramatically speeds up loading and picking operations.
We implement a strict multi-stage quality assurance protocol managed by 45 professional inspectors. Every batch undergoes raw material spectroscopic testing, automated robotic welding inspection, and precise load capacity evaluations complying with international industrial standards.
Yes. With 85 experienced R&D engineers, we offer comprehensive customization services including tailored height, depth, tier capacity, and full warehouse CAD simulation planning to meet unique operational requirements.
Thanks to our 18,500㎡ highly automated manufacturing facility and partnership network of over 850 suppliers, standard container production and dispatch are typically completed within 15 to 25 days depending on customization complexity.
 Maobang Storage