Explore our high-capacity industrial teardrop racking, heavy-duty boltless systems, and custom dynamic rolling shelves engineered for international logistics compliance.
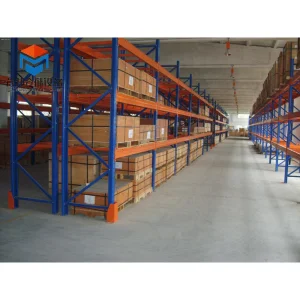

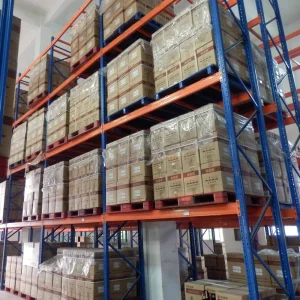
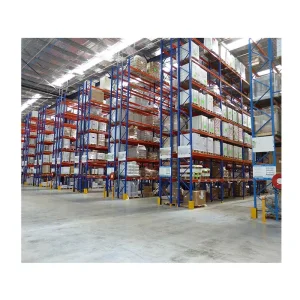
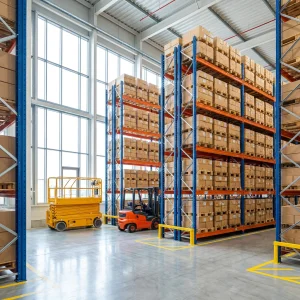
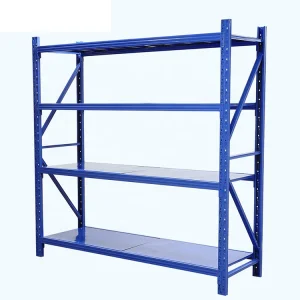
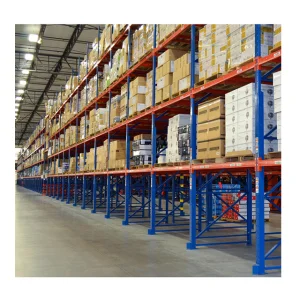
Analyzing global industrial real estate inflation, density optimization imperatives, and the evolution of mobile racking technologies across international markets.
In modern industrial logistics and material handling, real estate cost acceleration has altered structural warehouse design parameters globally. Logistics engineers, fulfillment center managers, and enterprise procurement directors face an escalating challenge: maximizing cubic floor utility while drastically minimizing operational footprint. Rolling shelves—often categorized as mobile racking systems, mobile shelving units, high-density movable storage, and track-guided lateral shelving—represent a paramount structural solution to this challenge.
Unlike conventional static pallet racking systems, which demand permanent access aisles between every storage row, engineered rolling shelves utilize dynamic base carriages mounted on steel tracks or guided via laser/optical systems. This structural design consolidates multiple operational aisles into a single moving aisle, unlocking up to 85% higher storage density without sacrificing direct access to stock keeping units (SKUs).
Across North America, Europe, Australia, and East Asia, warehouse leasing expenses have increased by 35% to 65% over the past five years. Implementing high-density mobile rolling racks reduces the required building footprint by 40% to 50% for equivalent pallet/carton capacities. This equates to substantial long-term operational savings in HVAC power consumption (especially in cold storage warehouses), civil construction costs, and property taxation.
Furthermore, global supply chain volatility has heightened requirements for customizable, rapidly deployable storage infrastructure. Enterprise procurement officers are shifting from standard off-the-shelf shelving toward OEM/ODM engineered racking systems capable of integrating automated guided vehicles (AGVs), RFID inventory monitoring, and specialized heavy-duty load profiles (ranging from 100kg light-duty archives to over 2000kg heavy-duty industrial pallet loads).
In-depth profile of a Tier-1 OEM/ODM manufacturing facility combining certified metallic metallurgy, automated roll-forming line capabilities, and rigorous international E-E-A-T compliance.
Guangdong Maobang Storage Equipment Co., Ltd. stands at the forefront of high-density industrial racking and specialized rolling shelf manufacturing in China. Established in 2016 (building upon 12 years of industry engineering experience and 7 years of dedicated international export operations), the organization has matured into a premier global supplier of intelligent warehouse equipment systems.
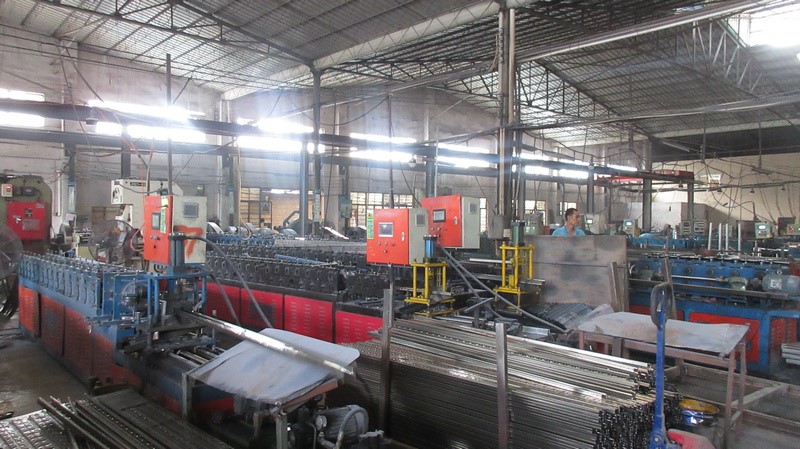
Headquartered in Guangdong's primary manufacturing hub, the company operates a state-of-the-art production facility covering approximately 18,500 square meters. Maobang achieved an annual export revenue milestone of USD 18 million, shipping precision-engineered storage systems to enterprise buyers across North America, Europe, Southeast Asia, the Middle East, South America, and Oceania.
| Key Organizational Parameter | Enterprise Data Benchmark | Global Industry Relevance & Buyer Value |
|---|---|---|
| Factory Scale & Footprint | 18,500 ㎡ Dedicated Facility | Enables massive simultaneous production runs and large-scale project staging. |
| Annual Export Output | USD $18,000,000+ | Proven global shipping reliability and international commercial contract execution. |
| Industry & Export Experience | 12 Years Industry / 7 Years Export | Deep understanding of international structural standards (FEM, RMI, AS4084). |
| Engineering & R&D Team | 85 Experienced R&D Engineers | In-house CAD/FEA simulation, tailored seismic load calculation, and custom structural CAD design. |
| Quality Control Department | 45 Professional Quality Inspectors | Full lifecycle testing: steel chemical composition, weld integrity, and coating thickness checks. |
| Supply Chain Network | 850+ Verified Partners | Guaranteed raw material (Q235B cold-rolled steel) sourcing and competitive pricing stability. |
| Product Innovation Rate | 120 New Products Launched/Year | Agile adaptation to automated warehousing trends, boltless assembly, and dynamic accessories. |
To support global supply chains, Maobang serves a broad industrial clientele encompassing warehouse operators, 3PL logistics hubs, automotive assembly factories, retail mega-chains, pharmaceutical distributors, and engineering contractors. Customization lies at the heart of Maobang's manufacturing philosophy—offering tailored dimensional sizing, customized load capacities (light, medium, to heavy-duty teardrop pallet racking), powder coating finishes, anti-seismic bracing, and complete end-to-end 3D warehouse layout planning.
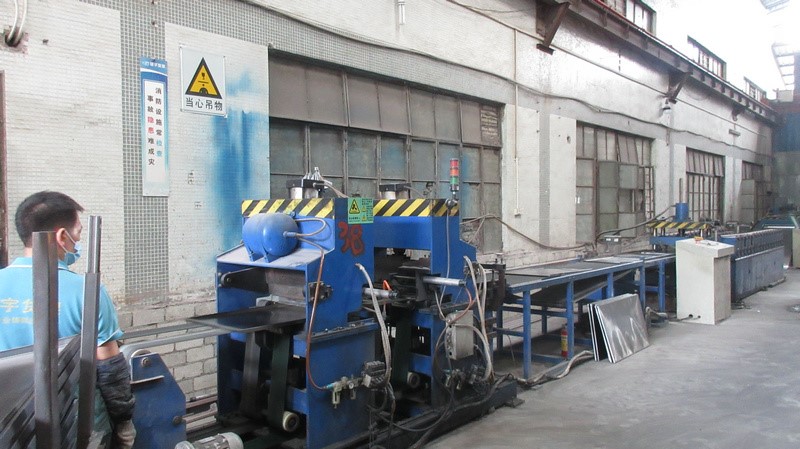
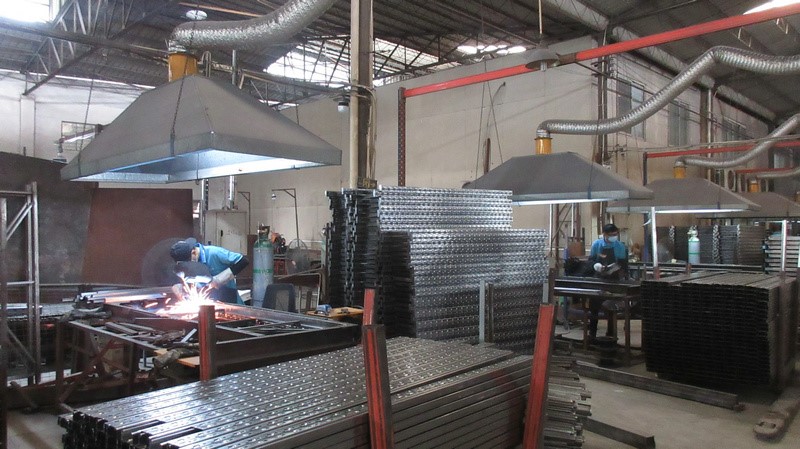
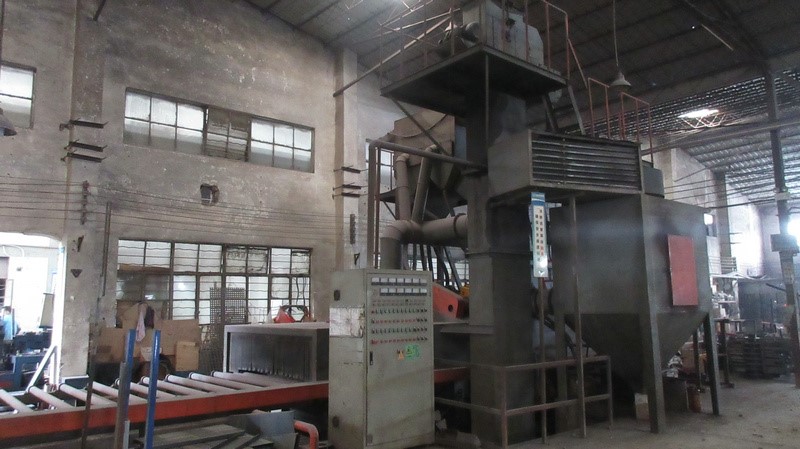
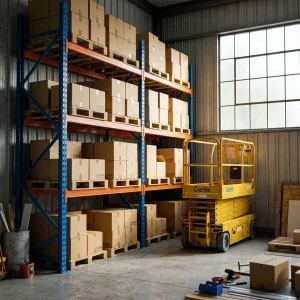
Visual verification of Maobang's advanced production pipeline—from raw material verification, cold-roll forming, robotic laser welding, to automated powder coating and multi-stage QC inspection.
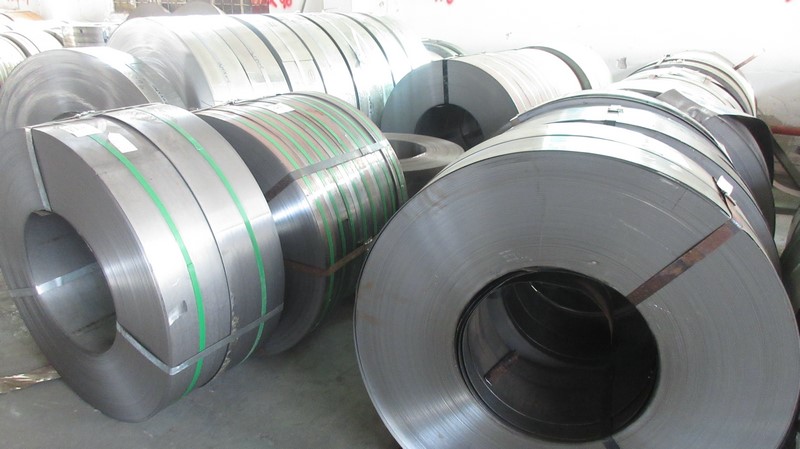
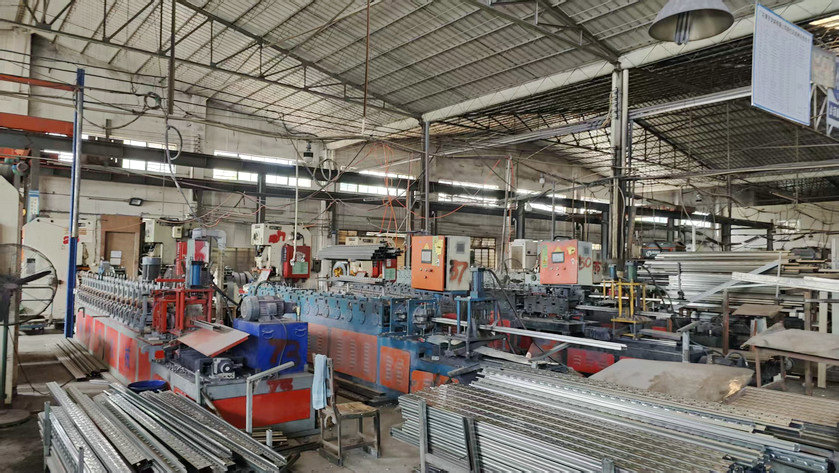
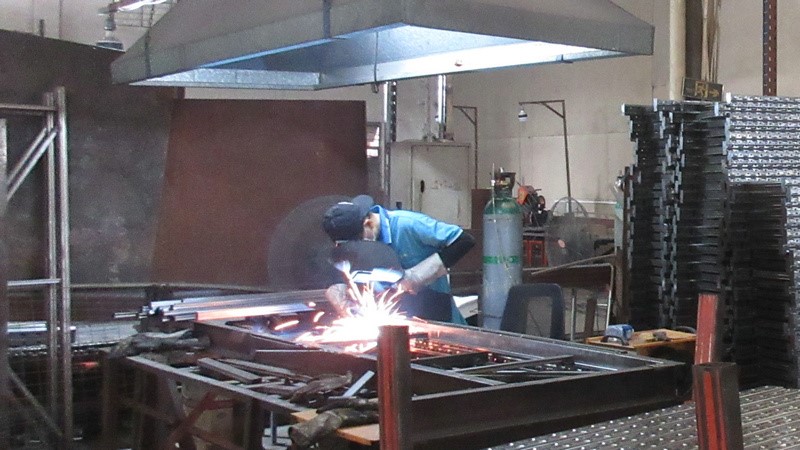
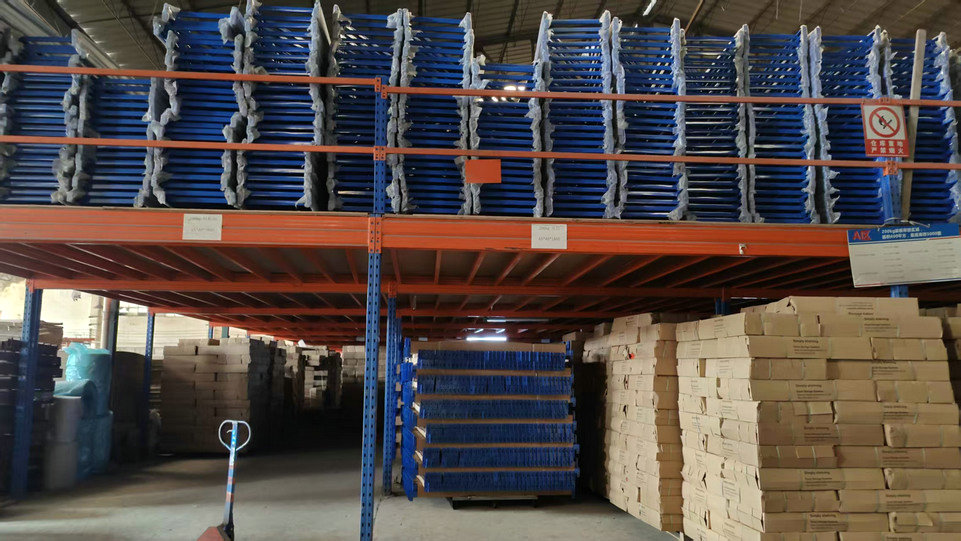
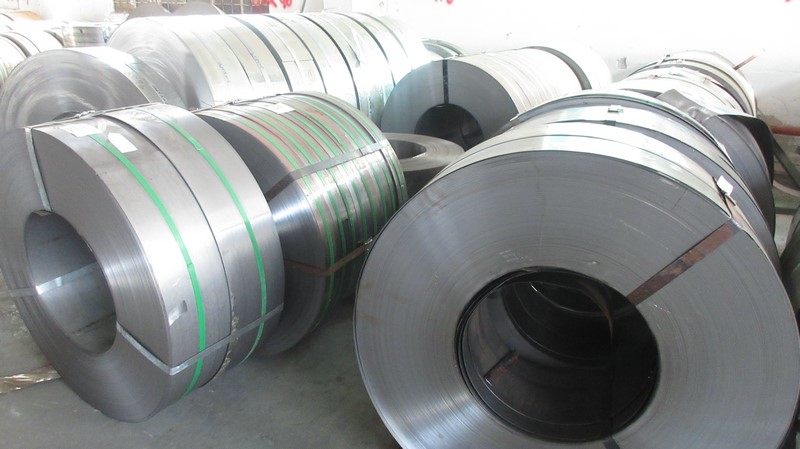
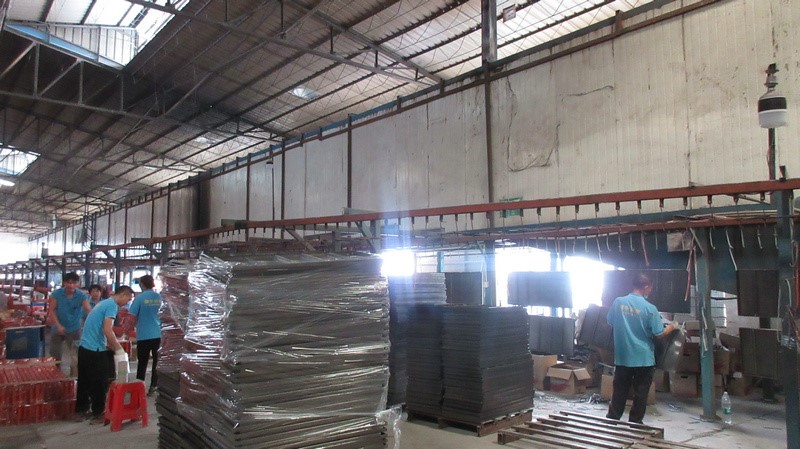
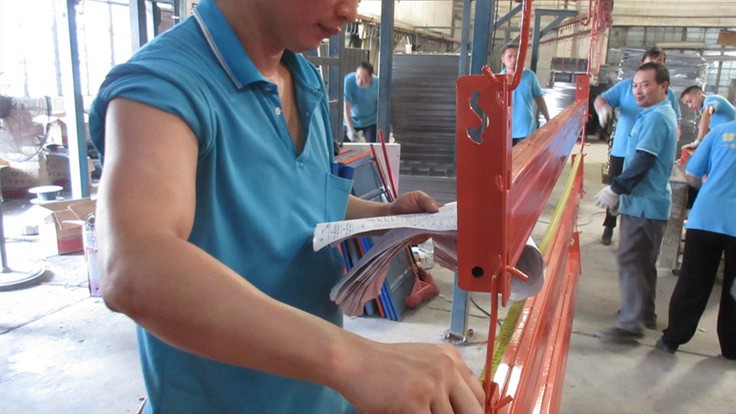
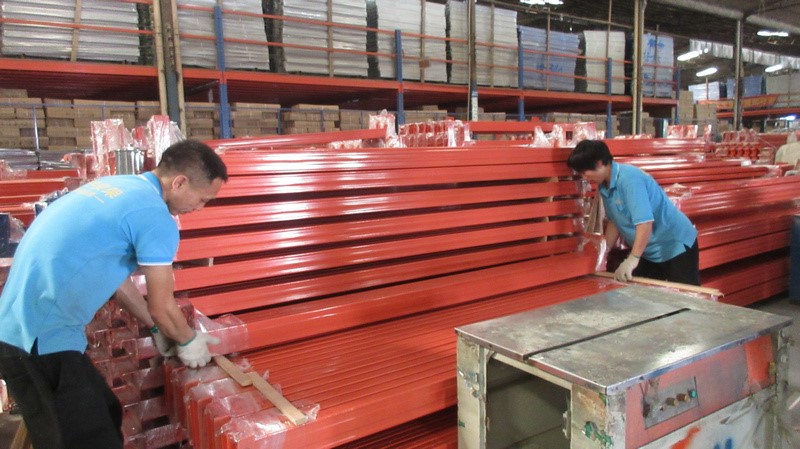
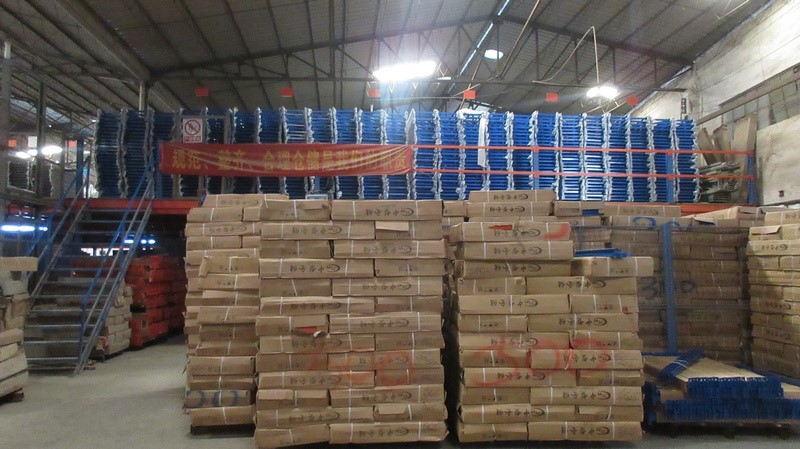
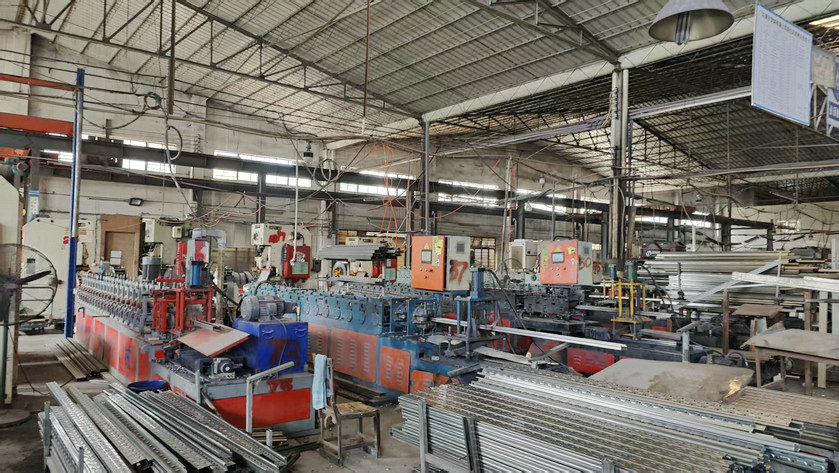
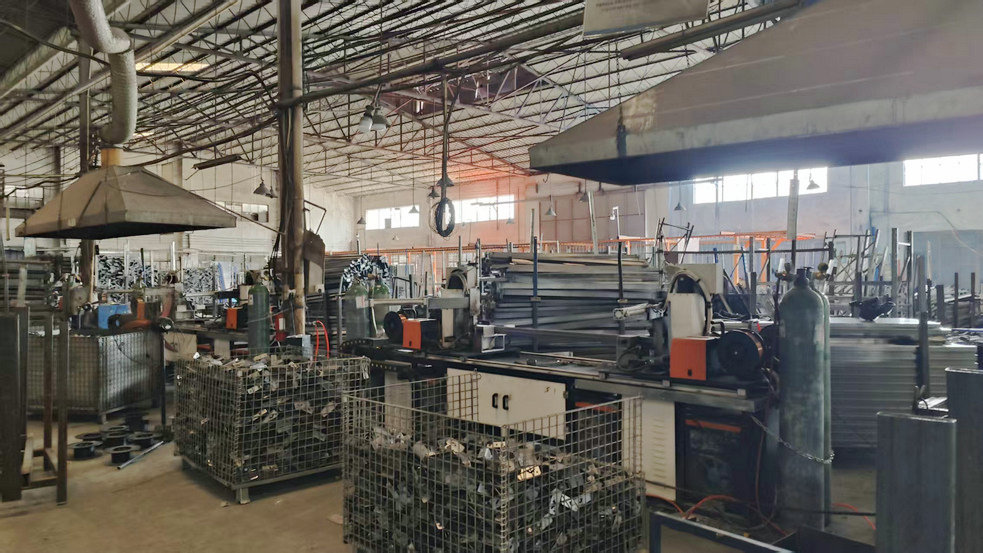
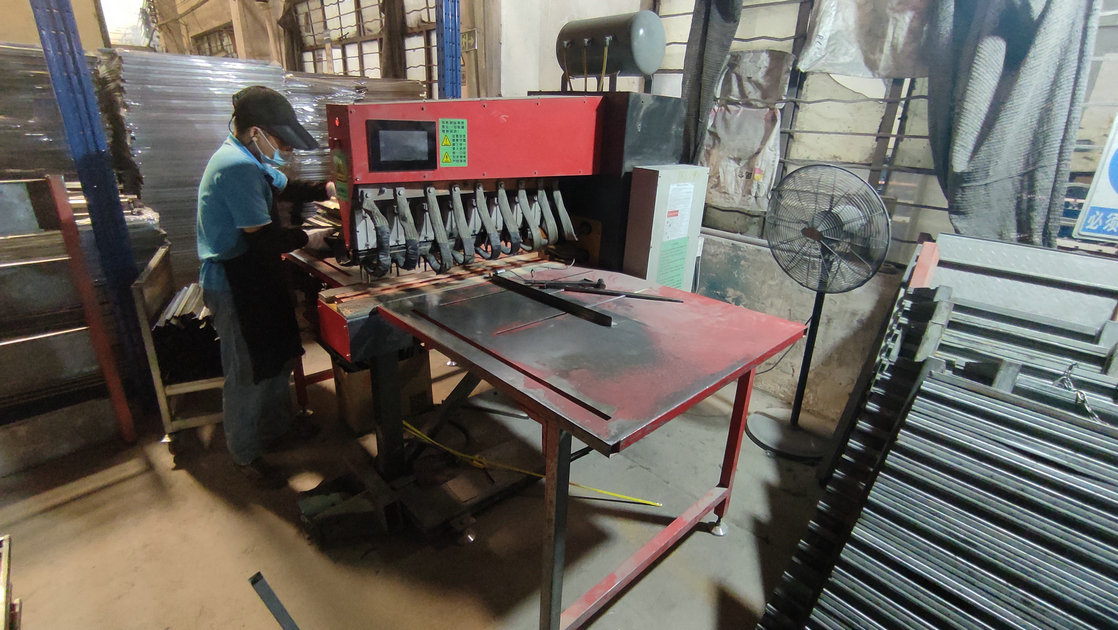
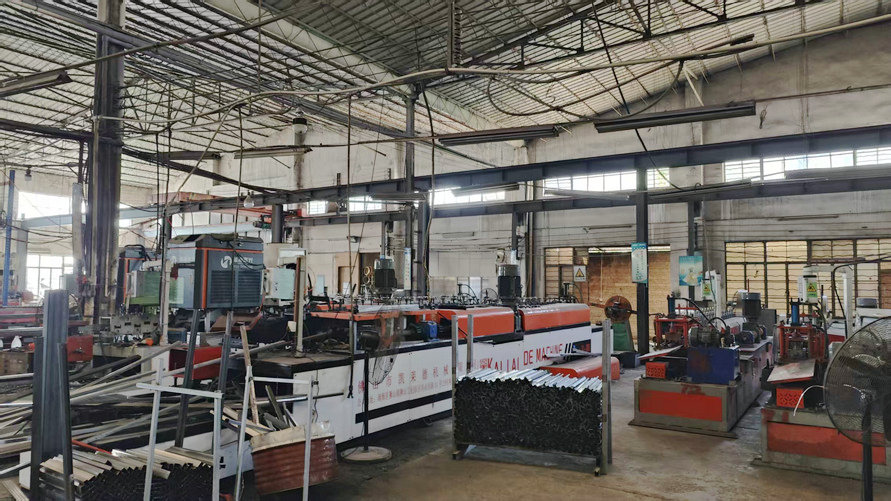
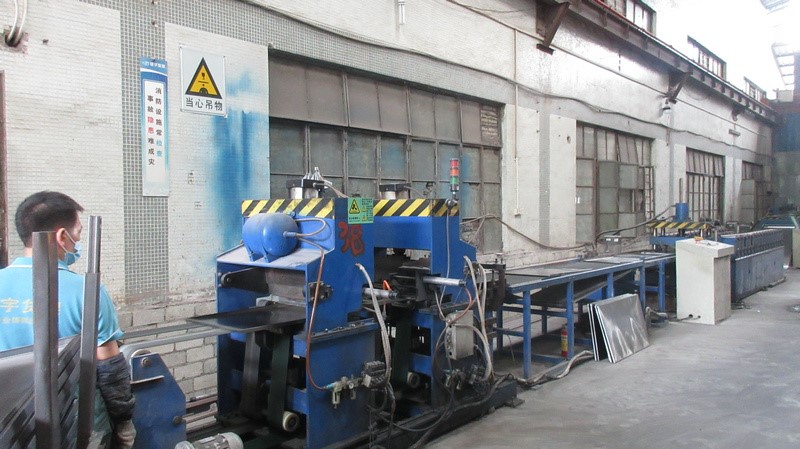
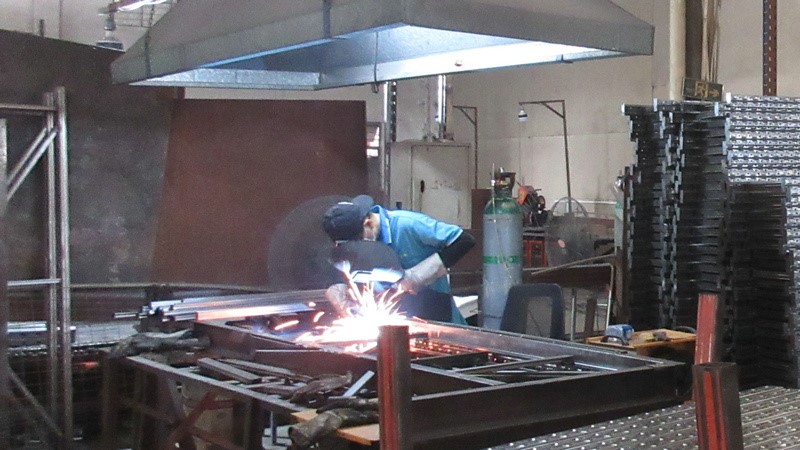
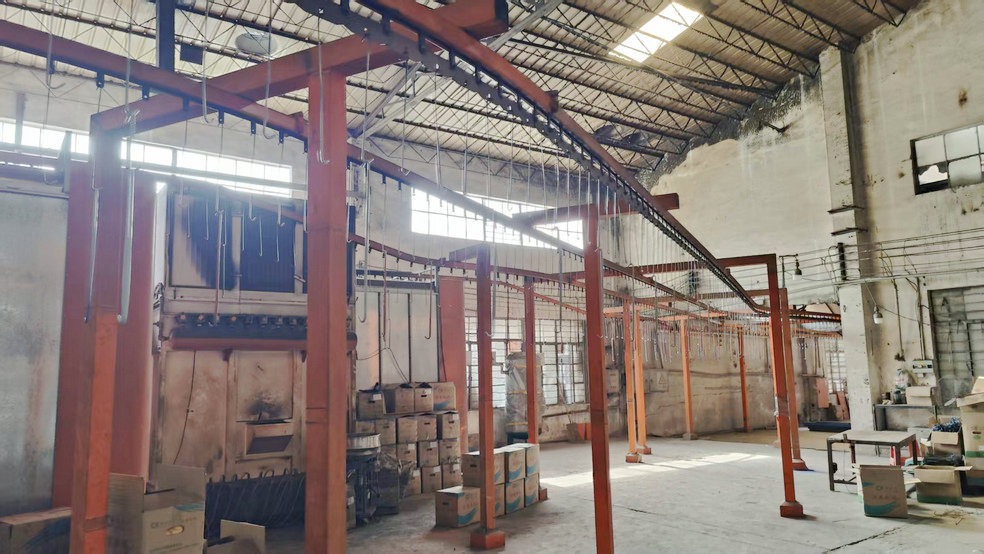
Technical breakdown of mechanical drive systems, load-bearing upright profiles, cold-rolled steel metallurgy, and modular racking configurations.
In high-density engineering, selecting between dynamic mobile rolling shelves and heavy-duty static pallet racking depends on structural load profiles, SKU accessibility requirements, and facility floor geology. Below is a comparative technical analysis compiled by Maobang’s senior engineering team:
Maobang utilizes high-strength Q235B cold-rolled structural steel across all load-bearing upright posts and box beams. The cold-rolling process enhances yield strength and dimensional consistency, preventing micro-torsional twisting under full load capacity. Furthermore, our continuous powder-coating spray line applies a 60–80 micron thick epoxy-polyester finish, ensuring maximum anti-corrosion protection in humid or temperature-controlled logistics environments.
How customized rolling shelves and heavy-duty storage racks solve critical space and logistics bottlenecks across major global industries.
In refrigerated facilities where electricity costs to maintain -25°C temperatures are extreme, wasted aisle space equals lost revenue. Mobile rolling pallet racks maximize cubic storage density, cutting total cooling volume requirements per pallet by up to 40%.
Rapid SKU turnover requires flexible multi-level medium-duty shelving and teardrop pallet systems. Boltless beam height adjustability allows operators to rapidly reconfigure shelf gaps as packaging dimensions vary with seasonal sales cycles.
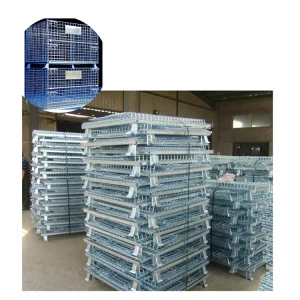
Heavy engine blocks, body stampings, and delicate components demand specialized storage. Wire mesh container stillages and double-sided heavy-duty racks provide high-visibility, stackable, and impact-resistant material management.
High-density mechanical rolling shelves allow financial institutions, hospitals, and government agencies to store millions of physical records in compact, dust-protected, and lockable mobile bays.
Heavy-duty 2000kg+ capacity beam racks designed with reinforced post-protectors safeguard against forklift collisions in manufacturing plants while storing heavy dies, molds, and metal stocks.
Light-duty widespan shelving and steel storage units offer clean, snag-free surfaces that protect apparel boxes, garments, and fragile consumer goods during fast-paced picking cycles.
Key structural metrics, safety certifications, container shipping optimization, and quality control guidelines for international buyers.
When enterprise procurement officers source industrial rolling shelves and heavy-duty racking from China, evaluating technical risk and supplier capability requires inspecting strict quality benchmarks. Maobang’s dedicated quality control department of 45 professional inspectors executes rigorous multi-stage protocols to mitigate risks:
The next evolution of mobile rolling racks in automated warehouse ecosystems.
The warehousing landscape is undergoing a digital transformation. Next-generation rolling shelves are transitioning from manual hand-crank systems to IoT-enabled smart mobile bases integrated with Warehouse Management Systems (WMS).
Key technological shifts shaping the next decade of industrial storage include:
Expert answers to critical procurement questions regarding custom dimensions, OEM/ODM services, load safety standards, and shipping lead times.
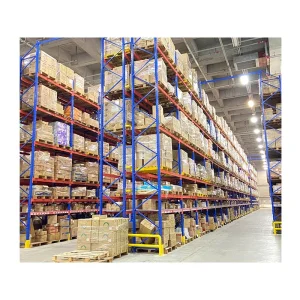
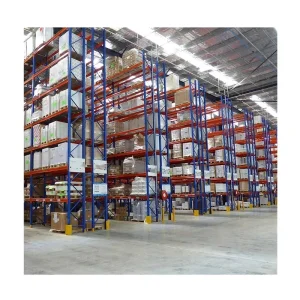
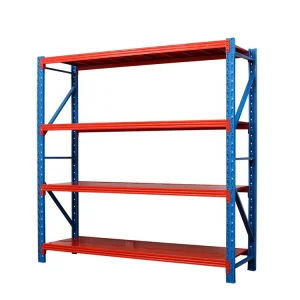
Discover heavy-duty metal pallets, wire mesh decks, selective beam systems, wide-span shelving, and high-load double-sided racking units.

 Maobang Storage